Mining is the application where cylinder selection most often goes wrong, and the mistake is almost always the same: the cylinder is chosen on force, and force is the one thing it will not fail on.
Duty cycle, not tonnage, sets the design
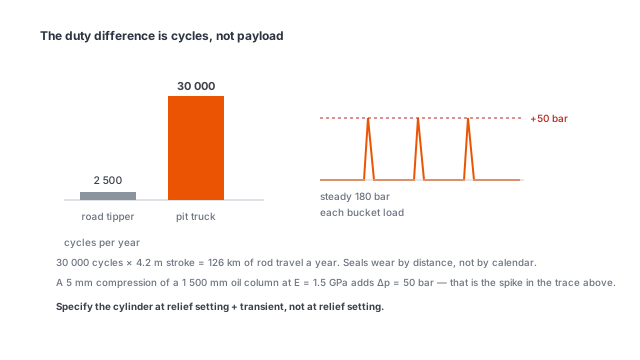
A road tipper tips 20 to 60 times a day. A haul truck on a mine site tips 400 to 700 times a day, six days a week. Multiply that by a 20-second cycle and the cylinder is doing the work of a road truck in the first three weeks of the year.
That changes which property matters. Seal life is a function of rod kilometres travelled, not force. A cylinder with a 900 mm stroke running 600 cycles a day moves the rod 540 metres per shift, and every metre drags the wiper over whatever the site is made of. The specification that decides whether the cylinder lasts a season or three years is the rod surface finish and the wiper design, not the bore.
Shock load is where the pressure rating is spent
Every time a loaded body reaches the end of stroke, the kinetic energy of the load has to go somewhere. It goes into the cylinder as a pressure spike, and on a tipping cylinder that spike routinely reaches twice the pump setting for a few milliseconds.
This is why a cylinder with a 180 bar working pressure and a 300 bar test pressure is not over-specified. The test pressure covers the spike the relief valve cannot catch. If a site reports cracked barrels or weeping base welds rather than rod seal leaks, the cause is usually a missing or badly set counterbalance valve, not a weak cylinder.
Rule of thumb: set the counterbalance 15 to 20 percent above the working pressure, and check it whenever the pump setting changes.
The four cylinder families that carry mining work
In dump and haulage duty, the choice is between underbody and front-end telescopic, exactly as on a road truck, but the capacity range shifts upward. Front-end telescopic covers 28.3 to 64 t in the FC series with 27 models, 4 to 6 stages and closed lengths from 1,195 to 1,945 mm. The FEE series covers 15.5 to 51.3 t of lifting weight in 9 models with 3 to 5 stages, and it is the lighter of the two families in mass for the same lift.
Where a body needs a shallow lift angle rather than a long stroke, the HTT scissor hoist covers 2.8 to 15.4 t with 3 to 6 inch bores and 10 to 30 inch strokes. That is utility and light haulage territory, not main-line haul truck duty.
For screens, feeders, drill rigs and maintenance cranes, the requirement moves to long stroke at moderate force. The HSG series runs 430 to 3,500 mm of stroke at 20 MPa with bore and rod combinations from 50/28 to 200/140 mm, which covers most plant-mounted applications where the cylinder is doing positioning rather than lifting.
What to put in the RFQ
Four things separate a mining quote from a general one:
- Cycles per shift and shifts per year. This is the only way to price seal life honestly.
- Contamination class. Whether the site runs ISO 4406 18/16/13 or worse decides whether the cylinder needs a boot and a double wiper.
- Mounting alignment tolerance. Mining brackets are welded in the field and are rarely within a degree. Spherical bearings at both ends absorb that.
- Rod finish. Induction-hardened rod at 50 to 55 HRC with 0.2 µm Ra chrome is the baseline; a 20 µm chrome on a soft rod will peel in a dusty environment.
Get those four right and the tonnage takes care of itself.
Start from the load case
If you have the body drawing and the cycle count, the cylinder falls out of the model tables in a few minutes. Send both, plus the pump pressure the machine already runs, and the answer comes back as a specific model rather than a range.